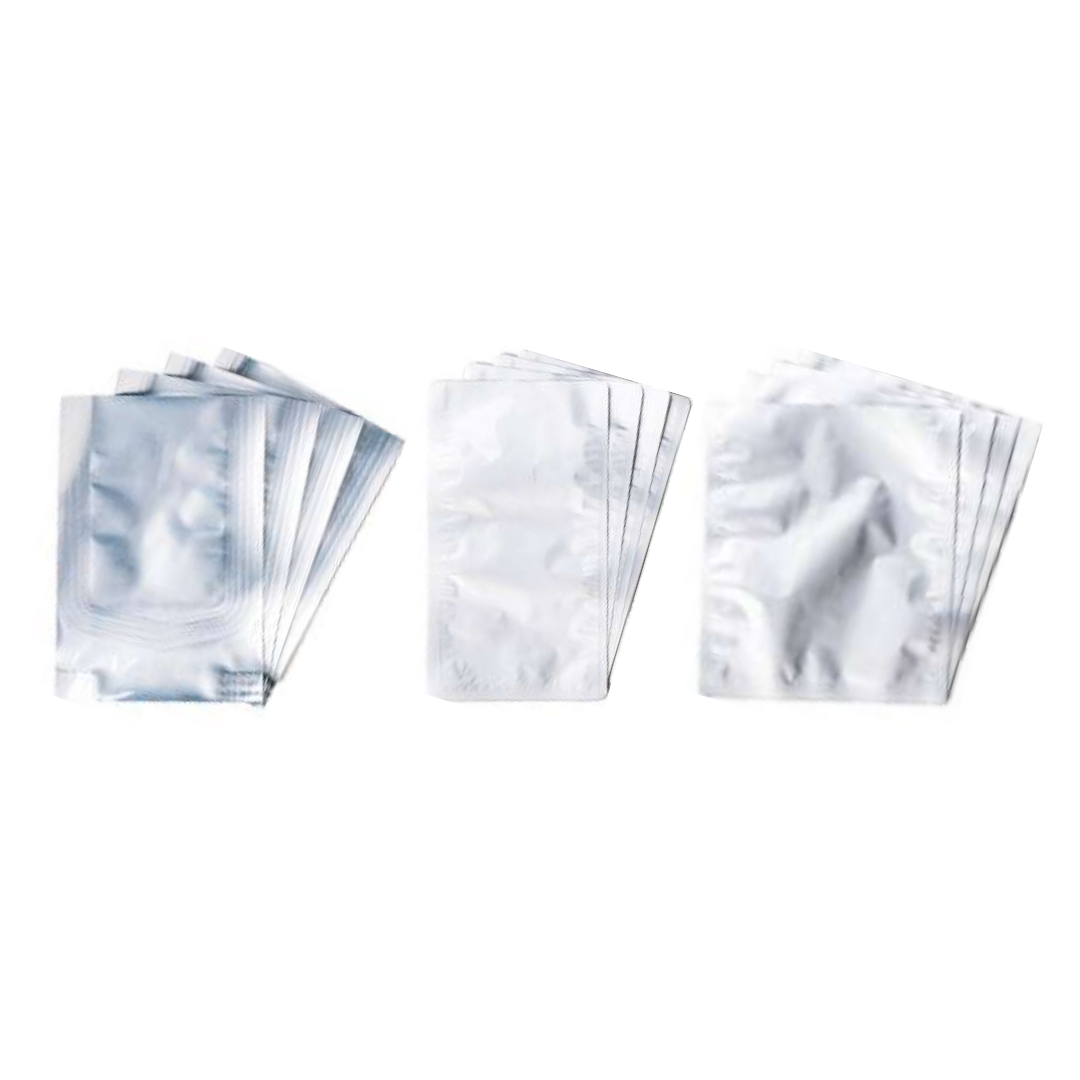
In the medical and pharmaceutical packaging industry, content protection is a key requirement. Barrier polybond offers advanced defense against moisture, oxygen, light and contaminants, preserving the integrity and safety of packaged products.
It is distinguished by its exceptional protective properties, making it a reliable and widely used solution for packaging medical devices, sterile products, and sensitive pharmaceuticals.
For maximum effectiveness and safety, this material offers a number of key advantages, including:
- Gas and Moisture Barrier
Polyacetal blocks the passage of oxygen (OTR – Oxygen Transmission Rate) and water vapor (WVTR – Water Vapor Transmission Rate), preserving product quality and sterility.
- Protection from light and contaminants
The barrier effect to UV light and external agents prevents chemical and microbiological changes, ensuring optimal preservation of the contents.
- Sterilisation compatibility
Polyacrylate is suitable for major sterilisation processes while maintaining its properties:
- ETO (Ethylene Oxide).
- Gamma irradiation
- Steam or Autoclave (when coupled with suitable materials)
- Mechanical strength and flexibility
Provides a balance between strength and manageability, protecting devices without compromising their ease of use.
The laminated barrier is composed of multiple layers of different plastics, either metallized or transparent, that together provide a level of protection similar to that of aluminium, while offering a more sustainable environmental impact.
The absence of aluminium enhances the product’s recyclability, allowing targeted recycling of the plastic film only.